Overview
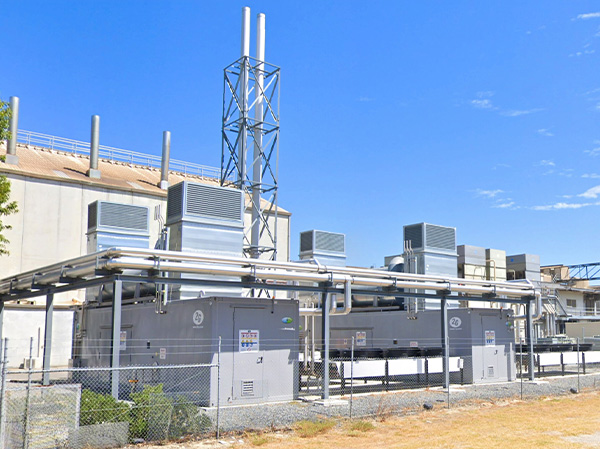
Our client operates a cheese manufacturing facility in Tasmania, where an anaerobic digester produces biogas from food processing waste. Raw biogas cannot be used effectively as it comes off the digester: left untreated, the moisture and hydrogen sulphide (H₂S) it carries will corrode equipment and reduce system efficiency over time. To condition the gas for safe, reliable downstream use, the client engaged Evo Energy Technologies to design, install and commission a complete biogas treatment system.

The system delivers
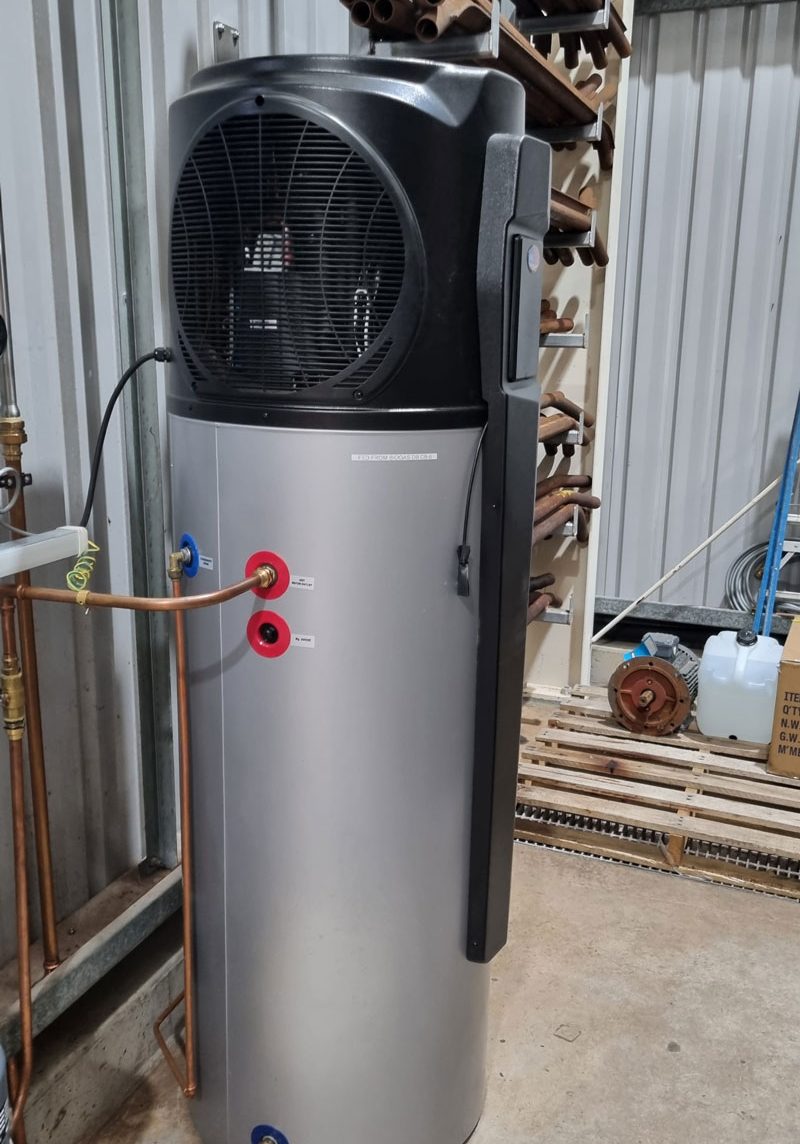
Evo Energy Technologies installed a 2G gas treatment system that first cools the incoming biogas to strip out moisture, then reheats it to lower the relative humidity to the level required for effective carbon filtration. The conditioned gas then passes through two activated carbon tanks in series, scrubbing hydrogen sulphide down to the concentration needed for safe downstream use. The reheat stage is supplied with hot water by an Evo270 hot water heat pump integrated into the treatment process, removing the need for a separate heat source for that stage.
The outcome
The facility now has a fully commissioned gas treatment system that conditions its biogas to a consistent, usable standard. Protecting downstream equipment from moisture and H₂S extends its working life and keeps the system operating at the efficiency it was designed for, letting the site draw full value from a fuel it produces on site.
Project Gallery